Mooch_Admin, Author at Erodex - Page 4 of 12
الفئات
دراسة حالة

التحسين المستمر يهيئ موردي صناعة الطيران للإقلاع بعد الجائحة

عانى قطاع الطيران في المملكة المتحدة من تحديات غير مسبوقة نتيجة للجائحة العالمية، وهي تحديات أثرت على الشركات الهندسية على كل مستوى من مستويات سلسلة التوريد، بما في ذلك الشركات الرائدة في السوق.

لحسن حظ إحدى الشركات الرائدة في مجالها، تزامن الاستثمار في برنامج التحسين المستمر قبل الجائحة مع متطلبات زيادة الكفاءة وخفض تكلفة كل جزء التي تتطلبها الآن صناعة تكافح من أجل التعافي.

هذا النجاح الذي حققه البرنامج لم يضمن فقط أن تكون الشركة في وضع أفضل لمواجهة العاصفة الحالية، بل خلق أيضاً فرص عمل جديدة بفضل العمليات الأكثر تنافسية وتطبيق التكنولوجيا المتقدمة.

James Kirk, Director of Operations at Erodex UK, the UK’s leading supplier of EDM graphite, graphite machining and tooling to the aerospace market, joined the company in 2019 to spearhead the CI drive.

وهنا يخبرنا المزيد عن الرحلة التي يقود فيها الشركة.

يقول كيرك: "نحن الآن في بيئة الآن في مجال الطيران حيث أصبحت تكلفة القطعة الواحدة أكثر أهمية مما كانت عليه قبل عامين".

"نحن مطالبون الآن أكثر من أي وقت مضى بإيجاد طرق أكثر كفاءة للإنتاج، وبالتالي يجب أن نتبنى التزاماً استراتيجياً بالتحسين والتغيير.

من الأسهل بكثير القيام بذلك عندما تقوم بذلك في شركة لا تحقق أداءً جيدًا. من الأصعب بكثير أن تأتي إلى شركة مثل Erodex، وهي شركة رائدة في السوق كانت تحقق أرباحًا وتنمو عامًا بعد عام وتقول "نحن بحاجة إلى التحسين".

ومع ذلك، هذا ما شرع كيرك، الذي يعمل مع زملائه المديرين والمالكين ستيف وإيان وجون رولينسون، في منشأة تصنيع الجرافيت في وينزبيري في ويست ميدلاندز.

"في البداية شرعنا في فهم الأداء الحقيقي للمنشأة. وحددنا إمكانية تحسين الالتزام بالتسليم ثم احتجنا إلى فهم الدوافع الكامنة وراء ذلك: هل كان ذلك يرجع إلى الأداء أو القدرة أو الكفاءة أو مزيج من هذه العوامل؟

يتابع كيرك قائلاً: "أصبح من الواضح تمامًا أنه كان هناك مجال لتحسين سير العمل وكفاءة التصنيع".

مع التركيز على المجالات ذات الأولوية لتحسين الكفاءة والجمالية وسير العمل في المتجر، تم الاتفاق على خارطة طريق للاستثمار في مجال التصنيع المتكامل بين المديرين والتي أعطت كيرك مجالاً واسعاً للاستثمار في المستقبل.

تضمنت المكاسب الأساسية والسريعة التي تم تحقيقها في العام الأول تحسين تخطيط المصنع، وإزالة الفوضى وتنفيذ بيئات خلوية للطحن والتصنيع الآلي. وقد أدى ذلك إلى خلق بيئة إنتاج أكثر مرونة وفعالية بكثير، وهو ما استكمل التحسينات الأساسية الأخرى مثل اللوحات البيضاء واجتماعات الفريق اليومية.

ويضيف كيرك: "بعد فترة من التقييم، ركزنا على تشجيع موظفينا على تبني التغيير والرغبة في أن يكونوا جزءًا من الرحلة، وضمان أن يكون لدينا العقلية والفلسفة الصحيحة للأشخاص في الموقع.

"لقد حاولنا أن نوضح لهم أنه من خلال التغيير، سيجعلون الأمر أسهل لأنفسهم وأفضل للأعمال. على سبيل المثال، من خلال رفع مستوى الفحص، وتحسين سير العمل بحيث تكون المواد جاهزة دائمًا مسبقًا للميكانيكي لبدء عمله التالي، والتأكد من فحص الأدوات. إن هذا النوع من الأساليب في التصنيع أساسي جدًا، ولكن بمجرد أن يقتنع الأفراد بهذه المبادئ الأساسية، يصبح من الأسهل عليهم المضي قدمًا في القفزات الكبرى".

أدى خفض التكاليف في البرامج الحالية من خلال فلسفة "مشغل واحد وثلاث آلات" لتعدد المهام وإعادة توزيع الأدوار والمسؤوليات إلى إرساء الأساس للاستثمار في آلات جديدة واستكشاف عمليات جديدة.

"نحن الآن في الطرف الأكثر تقنية من خارطة الطريق، حيث نقوم الآن بالتعمق في كل جزء على حدة في خطوط التشغيل وإعادة التشغيل ذات القيمة العالية. إذا نظرت إلى ما قمنا به في أحد خطوطنا ذات القيمة العالية، ستجد أننا حققنا بعض الوفورات الكبيرة في منتجاتنا. نحن نعمل الآن على تطوير تقنيات جديدة ونبحث الآن في مجال الروبوتات للمنتجات ذات الحجم الكبير".

"لقد بدأنا في طرح أسئلة جديدة، مثل "كيف يمكننا أخذ هذا الجزء الذي قمنا بتصنيعه آليًا في اتجاه ثلاثي المحاور وتصنيعه آليًا في اتجاه خماسي المحاور - وما تأثير ذلك على تكلفة القطعة الواحدة؟

"كما أن الاستثمار في الماكينات المختلفة مثل الماكينات خماسية المحاور وتعظيم قدراتها يفتح لنا المجال أمام منتجات وصناعات جديدة في المستقبل. وكشركة، أعتقد أننا بدأنا ندرك أنه على الرغم من أننا رواد الصناعة فيما نقوم به، إلا أننا نستطيع أن ندفع بأنفسنا إلى النمو في مجالات جديدة أيضًا، وهناك جوانب من تصنيع الأقطاب الكهربائية في مجال الفضاء الجوي لم نتمكن من القيام بها لسبب أو لآخر في الماضي، لأسباب تكنولوجية بشكل أساسي".

وتعتقد الشركة أن برنامج التوسع الذي تبلغ تكلفته 1.75 مليون جنيه إسترليني سيضمن لها أن تكون في أفضل وضع للاستفادة من التحسن الاقتصادي المتوقع خلال عام 2021 وما بعده.

وقد أدى الاستثمار في الماكينات الجديدة إلى زيادة الطاقة الإنتاجية في الموقع بنسبة 40 في المائة، ومكّن الشركة من الحصول على عقد لقطعة لم تكن قادرة على المنافسة عليها في السابق خلال أول أسبوعين من وجود الماكينة الجديدة في الموقع.

ويقترن ذلك بالاستثمار في فريق عمل متنامٍ يتبنى رؤية كيرك ومديري Erodex للمكان الذي يتجه إليه كيرك ومديرو Erodex.

"لدينا فريق عمل ملتزم حقاً بما نقوم به. نحن نستثمر في موظفينا، ونعمل على تطوير المواهب الشابة داخل الشركة، وبالنسبة لي، فإنك تحصل على استجابة أكثر استباقية إذا كان لديك مزيج أكثر ديناميكية من المواهب ضمن القوى العاملة لديك.

ويختتم كيرك حديثه قائلاً: "إنها مجرد حالة من الدفع المستمر إلى الأمام".

إذا كنت مهتماً بمعرفة المزيد، يُرجى الاتصال بنا.
الفئات
الأخبار

Erodex support Krohne with design and manufacture of fixture for UK’s largest horizontal vacuum furnace

KROHNE is a world-leading manufacturer and supplier of solutions in industrial process instrumentation. Within the UK, KROHNE Ltd is the group’s global centre of excellence for Coriolis mass flowmeter technology. Its manufacturing plant in Wellingborough is where the award winning OPTIMASS range of mass flowmeters is produced.

The process of manufacturing products at Krohne Ltd often involves working with specialist materials such as Duplex 31803 and Super Duplex 32750 stainless steels. Particularly with regards to materials such as Super Duplex, it is highly critical that the brazing process is completed correctly.

However, the largest of Krohne’s products to be brazed are up to two metres in length and no suitable furnace exists within the UK that has the hot zone capability to process such a large product.

This meant that the brazing of this product was subcontracted to a supplier in France, which brought challenges with lead times, transport, and associated cost issues.

The objective: bringing the brazing process in-house.

Krohne Ltd’s Management team made the decision to bring the process of brazing their larger products in-house, thus ensuring complete control over quality and lead times.

Following a significant investment in the UK’s largest horizontal vacuum furnace, the company required assistance with the design and manufacture of a fixture that would possess the specific hot zone capability, be of appropriate size and at the same time cope with weight, cost and distortion limitations whilst processing the larger Krohne Ltd products.

For this, the Krohne Team turned to Erodex UK.

Evolution of fixture design

Discussions started around six to nine months prior to when the furnace was due to arrive. The original concept design provided by the Erodex UK team was based around using graphite plates and spacers.

Following close consultation with their Krohne counterparts this was reviewed and it was determined that a flat grid method would be more suitable, due to strength requirements of the fixture and to enable the required reduction in fixture weight.

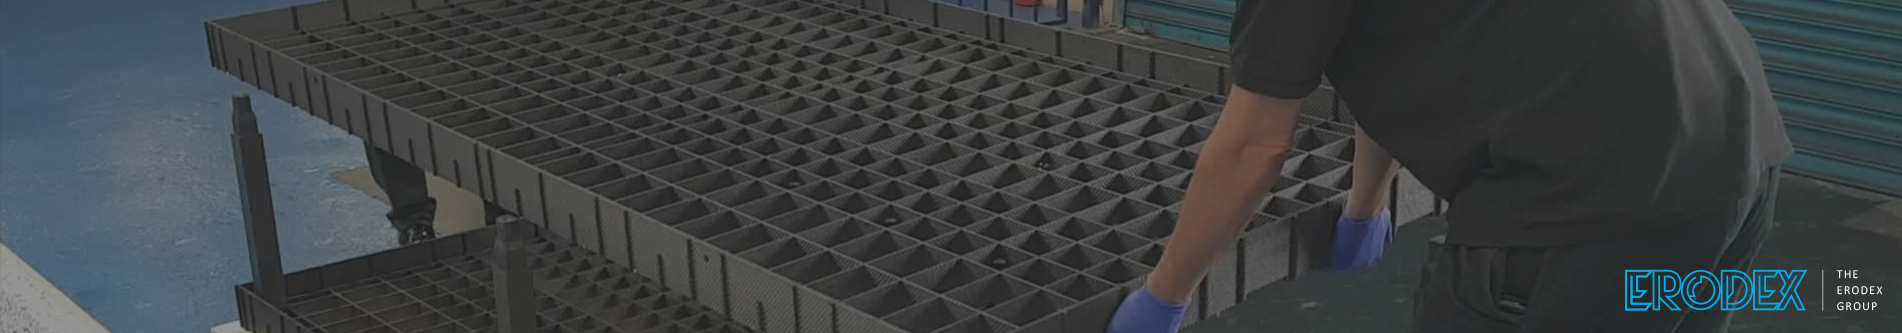
The resulting design was a 2.4m x 1.2m Carbon Fibre Composite (CFC) fixture consisting of 2 layers and a cover plate to ensure that there was no direct radiation heat onto the components processed on the top layer and that heat is evenly distributed within the furnace.

Production Engineering Manager Darren Hawes comments: “The Erodex team were able to understand our specific requirements and design a fixture based on a CFC grid. We then had a further meeting and added in channels and a cover plate that sits on top of the CFC grid structure to maintain 0.1mm flatness.

“Perforated holes were added to allow the 360-degree gas cooling to flow underneath the fixture to the parts, because cooling is one of the critical features of the process. Side rails were added to the fixture to remove the possibility of any parts falling off and we added lifting points to the fixture, so once removed from the furnace, if the loader were to break down at any point, the fixture could be removed from the loader by overhead cranes”.

Andrew McFarlane, Technical Sales Engineer at Erodex UK and project lead adds: “When it became clear that a more intricate and technical design was required, we involved our full High Temp team and further meetings took place to come up with the optimum design to incorporate the changes our customer identified and to deliver the additional required project features such as spares and changes to the spacers.

“We showed flexibility to provide what the customer wanted to achieve this and altered the designs until they were satisfied”.

Why was Carbon Fibre Composite (CFC) graphite the material of choice for fixture manufacture?

Durability properties such as their high strength, stiffness, high thermal shock resistance and high fracture toughness, combined with being lightweight and having low rates of thermal expansion, CFC is the optimum material solution for charging systems in vacuum furnaces

Erodex CFC is available in a range of grades starting with Standard, for heating elements and furnace linings, Premium which is utilised for heating elements and structural components, Performance, for charging frames and systems, Filwound for cylinder components and Mechanical for connection elements.

Krohne Ltd Manufacturing Engineer Tom Harrison explains why, guided by the Erodex UK team, they opted to manufacture the fixture from Carbon Fibre Composite (CFC) graphite: “We had to find the right material for the fixture when considering weight, cost and distortion limitations and we could not find another material that was comparable to CFC for achieving this.

“The CFC fixture is lightweight yet as the temperature increases within the furnace the material gets stronger. Our main requirement of the fixture and the plate itself was to have a 0.1mm flatness tolerance, so when we manufacture and process our parts, any distortion of the fixture does not impact on the assembly that is being processed.

“The straight tube assemblies being processed within the furnace also have a 1/600mm straightness tolerance. Up to two metres we can have 3mm distortion end to end in the bow of the tube. To get that right, we required the fixture base to be as true as possible, so that we are not adding any additional distortion into the processing of the parts. The CFC fixture was therefore designed and manufactured by Erodex to deliver on that 0.1mm flatness constraint.

“In addition, the more mass within the furnace, the greater the effect on heating and cooling rates. A metallic fixture can act as a heat sink, using CFC reduces the mass greatly so our process is optimised and the energy we do use is used efficiently”.

Additional benefits of using a CFC grid structure.

An added benefit of a CFC grid structure is that if individual parts of the fixture break, only these need to be replaced. This contrasts with a metallic grid, where the whole grid would need to be replaced or refurbished, resulting in a significant reduction in maintenance costs.

Furthermore, Duplex stainless steel and Super Duplex stainless steel are mainly used for corrosion resistance, meaning that any carbon or other contamination picked up from the fixture itself could affect the metallurgy of the material, which in turn can add further complications to the products being processed.

To avoid this, the CFC graphite fixture was coated in a Yttria Zirconia coating to prevent any carbon ingress into the material.

Hawes continues: “The knowledge of the application and properties of CFC within the Erodex UK team was vital in helping us to understand what could be achieved both with the material and the fixture design itself. As we moved through the process, the design became more complex, so having their expertise at hand to help develop this was very beneficial to us.

They acted like a partner on this project, and it was clear from the outset that they were willing to listen, accommodating changes and providing new ideas”.

Fixture assembly and operation.

Erodex assembled the fixture prior to coating and provided a video demonstrating how this should be repeated. Following coating of the fixture, the team were back on site to reinforce this with demonstrations of the ease of assembly to all Krohne Ltd end users.

Hawes’ team need to make sure the fixture is precisely central within the furnace every time it is loaded. To achieve this, a specialist forklift is used and Erodex designed the fixture to be held by the forklift so that this was achievable. The forklift is centralised as you drive it into the furnace, by two guides that sit underneath it.

Harrison adds: “The fixture itself has been used now since October, we have completed numerous cycles and it is holding up to design requirements of flatness, the coating is performing well and ultimately, the fixture is achieving what it was required to do.

“We vacuum clean the fixture and furnace after every cycle to remove any debris coming from the processing. The fixture also goes through a maintenance check/ two weekly burnout to remove any contaminants that may have come onto the fixture because of the processing of the products in the furnace.

“We have also used the CFC graphite fixture to process a product as part of our furnace validation that was previously processed by a subcontractor. We could see that there was 7mm distortion end to end on the part provided by the subcontractor. Once we processed it through on the fixture all the contact points were then level again. We would have not been able to achieve that in a subcontract furnace.

“Ultimately, this has given us full control over processing. It has given us the capability to develop our processes and increase productivity and allows continuous development and improvement of the process too.

“For example, we had identified a few issues with how one cycle was run, where we were positioning the monitoring thermocouples to ensure the parts are fully up to temperature before we started the brazing part of the process, so it has given us further knowledge on that, which in turn has benefitted the product being processed”.

For more information, please contact us

الفئات
الأخبار

World’s fastest brass wire launched by Erodex UK.

Betterbrass, the world’s fastest brass wire, launched by Erodex UK, has helped users increase cutting speed by up to 10% in early trials.

Launched in the UK this summer, Betterbrass is a next-generation special-alloy brass wire from Bedra (Berkenhoff) in Germany.

Thanks to innovative alloy and casting technology, along with a specially developed annealing process, Bedra engineers created a brass wire electrode comprised of a completely new alloy that is plug-and-play on all machine types. The new product delivers performance never before seen in traditional brass wire, with reported cutting speeds up to 10% faster.

“Since its launch earlier in the summer, the new betterbrass wire range has received a positive response from customer trials, meaning that we can now provide EDM subcontractors with a cost-effective step up from standard brass wire”, comments Josh Bye, Sales Engineer at Erodex UK.

“As UK industry starts to recover from the effects of the Covid-19 pandemic, we were keen to be able to introduce a new, cost-effective wire to the market that also enables increased performance. Users will save money by using the wire, as any increase in wire speed ultimately means less wire usage,” continues Bye.

Erodex UK is the market leader in providing EDM wire, wear parts, and other EDM consumables, and has cemented its position as the UK’s leading authority on all things EDM. In addition to their vast experience in the EDM industry, this is due to their strong working relationship with Berkenhoff (Bedra) in Germany.

During August 2019, Erodex UK announced the launch of the world’s fastest EDM speed wire, gapstar ONE. Building on the strengths of their cobracut, broncocut and topas ranges, Bedra developed a new coating technology called TRIMPAC. gapstar ONE quickly became the wire of choice for those looking for premium performance. Still, it is a different segment of the market that Erodex UK believes will continue to benefit from the betterbrass range.

“Being the fastest EDM speed wire available in the world, our gapstar ONE range is a very high-end wire, which we do advise if people are looking for a significant step up in speeds. However, we know that there is a segment of the market that does not demand premium performance but still wants greater performance and reliability than they get from standard brass wire. It is these users who are now appreciating the benefit of the new BetterBrass range of wire.

“During customer trials since launch, BetterBrass has proved to perform up to 10% faster than standard brass wire. Being a stronger wire than standard brass also means improved reliability when auto wire threading. Users have reported fewer breakages when applying increased power through the wire and better surface finishes too,” adds Bye.

Luke Hobbs, Director of HLP Engineering Solutions in Halesowen, West Midlands, has experienced firsthand the benefits of using both the gapstar and betterbrass ranges.

“We’ve used both Gapstar and BetterBrass wires from Erodex. Simply put, Gapstar is the best wire we have ever used for performance and speed on our Sodick machines. We found it ideal for cutting punches and other long-running jobs. We will have no hesitation in using Gapstar for this type of work in the future. We found that better brass is excellent for threading and, for the small increase in wire cost, offers a decent speed improvement of around 10-12% over standard brass wire with the same settings. When the job dictates, we will certainly use this wire again”.